Water and other liquids can collect in low areas of industrial facilities. If they remain there for too long, they can affect equipment and daily operations. Sump pumps help remove these liquids and keep working areas under control.
Sump Pump Manufacturers design pumping solutions for different industrial conditions. These pumps can support drainage, wastewater handling, chemical transfer, and other applications. However, the right pump depends on the liquid, sump depth, flow rate, and working environment.
Malhar Pump offers sump pump solutions for industrial applications. Its current product range includes sump pumps designed for industrial use, along with options for demanding applications.
What Is a Sump Pump?
A sump pump is designed to remove liquid collected in a sump or low-lying area. The pump transfers the liquid to another location through a suitable discharge line.
Industrial facilities may use sump pumps to handle wastewater, process liquids, drainage water, and other fluids. The pump design depends on the type of liquid and the conditions around the sump.
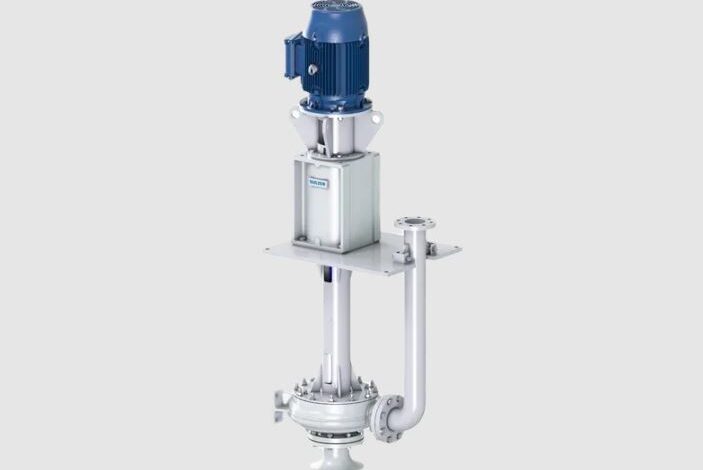
Vertical sump pumps can also help save floor space. Malhar Pump lists vertical sump pump designs for industrial applications.
Sump Pump Manufacturers may offer different designs based on flow, head, material, and application needs. Therefore, businesses should review their requirements before selecting equipment.
Why Sump Pumps Are Important
Liquid buildup can create several problems in an industrial facility. It can make floors slippery and affect nearby machinery. In some cases, it can also interrupt production.
A suitable sump pump helps remove collected liquid before it becomes a larger issue. It can support cleaner work areas and better liquid management.
Sump pumps are useful in several applications, including:
- Industrial drainage
- Wastewater handling
- Chemical processing
- Filtration systems
- Pollution control
- Manufacturing plants
- Mining operations
- Process industries
Malhar Pump also lists sump pump applications involving sewage, slurries, corrosive chemicals, and acidic water.
How to Choose the Right Sump Pump
Choosing the right pump starts with understanding the application. First, identify the type of liquid that needs to be pumped. Water, slurry, chemicals, and wastewater can have very different pumping requirements.
Next, check the required flow rate. Flow rate determines how quickly the pump needs to remove the liquid. Pump head is also important because it shows how high or far the liquid must travel.
Sump depth is another factor to consider. A deep sump may require a different pump configuration than a shallow sump.
Before choosing equipment from Sump Pump Manufacturers, consider:
- Type of liquid
- Required flow rate
- Pump head
- Sump depth
- Liquid temperature
- Solid content
- Material compatibility
- Operating hours
- Installation conditions
- Maintenance requirements
These factors can help businesses avoid selecting a pump that does not match their system.
Common Industrial Applications of Sump Pumps
Sump pumps can support many industrial processes. Their exact use depends on the liquid and operating conditions.
Manufacturing plants may use them to remove water or process liquids from collection pits. Wastewater facilities can also use sump pumps for liquid transfer and drainage.
Chemical industries may require special materials when handling aggressive liquids. For example, Malhar Pump lists stainless steel, polypropylene, and vertical cantilever sump pump options for different applications.
Mining and mineral processing can also create demanding pumping conditions. Slurries and changing loads may require specially designed equipment.
Therefore, Sump Pump Manufacturers need to consider the application before recommending a suitable design.
Benefits of Using Industrial Sump Pumps
A suitable sump pump can make liquid management easier. It can help prevent water buildup and reduce the risk of interruptions.
Vertical designs can also help save valuable floor space. This can be useful in busy industrial areas where equipment placement matters.
Some heavy-duty designs are built for long operating periods. Malhar Pump states that its double-bearing sump pump is designed for heavy loads, high vibration, and continuous-duty applications.
Other potential benefits include:
- Better liquid management
- Reduced water buildup
- Space-saving installation
- Support for continuous operation
- Suitable options for demanding liquids
- Easier system planning
However, the actual performance depends on correct sizing, installation, and maintenance.
Maintenance Tips for Sump Pumps
Regular maintenance helps keep a sump pump working properly. Operators should inspect the equipment according to the manufacturer’s recommendations.
Start by checking for unusual noise and vibration. These signs may indicate wear or another mechanical issue.
The pump and discharge line should also remain clear. Blockages can reduce flow and place extra stress on the equipment.
Simple maintenance steps include:
- Inspect the pump regularly.
- Check for unusual vibration.
- Monitor pump performance.
- Keep the discharge line clear.
- Inspect seals and connections.
- Check for visible damage.
- Follow the recommended service schedule.
- Record maintenance activities.
Regular inspections can help identify problems early. As a result, businesses can reduce the chance of unexpected downtime.
Why Material Selection Matters
The material used in a sump pump should match the liquid being handled. This becomes especially important when the pump works with chemicals, acidic liquids, or abrasive materials.
For example, stainless steel may suit some applications where corrosion resistance is important. Polypropylene can be useful for certain chemical environments.
Malhar Pump lists different sump pump configurations for applications involving corrosive chemicals, acidic water, sewage, and abrasive or solid-laden liquids.
Therefore, businesses should share complete application details with Sump Pump Manufacturers before selecting a model.
Role of Professional Sump Pump Manufacturers
Industrial pumping systems often require careful planning. The pump must work properly with the sump, piping, motor, and discharge system.
Professional Sump Pump Manufacturers can help businesses evaluate these requirements. They can consider flow rate, head, sump depth, liquid characteristics, and operating conditions.
Malhar Pump states that its engineering team can review load conditions, vibration levels, sump depth, and flow rate when recommending a suitable sump pump.
This application-based approach can help reduce selection errors. It can also support better performance after installation.
Frequently Asked Questions
1. What is a sump pump used for?
A sump pump removes liquid collected in a low area or sump. Industries use these pumps for drainage, wastewater, chemicals, and other applications.
2. Where are sump pumps commonly used?
They are used in manufacturing plants, wastewater facilities, chemical industries, mining sites, filtration systems, and other industrial locations.
3. How do I choose a sump pump?
Check the liquid type, flow rate, head, sump depth, temperature, solid content, and material requirements before selecting a pump.
4. Can sump pumps handle chemicals?
Some sump pumps are designed for chemical applications. However, the pump material must be compatible with the specific liquid.
5. Why is regular sump pump maintenance important?
Regular maintenance can help detect wear, blockages, vibration, and other problems early. It can also support reliable operation.
Conclusion
Sump pumps play an important role in industrial liquid management. They help remove collected liquids from low areas and support smoother daily operations.
The right pump should match the liquid, flow rate, head, sump depth, and operating environment. Material selection also matters when handling chemicals, slurries, or corrosive liquids.
Sump Pump Manufacturers provide different designs for different industrial requirements. Malhar Pump offers sump pump solutions for applications ranging from drainage to demanding chemical and process environments.
If your facility needs a sump pumping solution, first review the liquid and operating conditions. Then, discuss your requirements with a qualified pump supplier to select suitable equipment.